Table of Contents
Fluted Plastic Boxes: Repeated Fold and Assembly Trials addresses a specific B2B decision: crease geometry and assembly sequence. The right choice depends on the finished application and the way it is handled, not just the product name. Use the checks below to compare samples, prepare a clear request for quotation and approve a repeatable supply specification.
The decision for fluted plastic boxes
The practical starting point is a return loop that repeatedly collapses and rebuilds boxes. The risk is specific: fold lines fatigue before the packaging is retired. A decision about fluted plastic boxes should therefore begin with crease geometry and assembly sequence, rather than a comparison based only on a photograph or the nominal material name. This article sets out a qualification and purchasing method for that situation. It does not assign a universal load rating, service life or certification to an unspecified grade.
A useful acceptance statement is that the box continues to assemble and close without damaged creases. Translate that statement into a short inspection record before asking for quotations or changing the current design. Decide who will observe the result and which product condition must remain unchanged. Where a drawing dimension is involved, agree the measurement position and method. Where appearance or handling matters, retain a physical reference or a clear operating example.
The first trial should cycle a sample through the actual fold-flat and erecting routine. Keep the actual product, its support arrangement and the relevant operating sequence in the comparison. Record the sample code, drawing revision, conditions and observations together. If a detail is changed during the trial, identify the revised sample separately. This makes it possible to distinguish a useful improvement from a different setup that was never compared fairly.
The most informative failure to investigate is the one connected to crease geometry and assembly sequence. Photograph the relevant area before and after the trial and record whether the problem appeared during preparation, operation or unpacking. Do not merge distinct failure causes into one rejected-sample count. That distinction helps determine whether the next action belongs in material selection, conversion, packing or the working method.
For the order, keep crease geometry and assembly sequence visible in the drawing or acceptance sheet. Ask the supplier to identify any proposed deviation before production. The release decision should refer to the sample and evidence that were actually reviewed. An appealing prototype is a starting point; repeatability in the supplied batch is what allows fluted plastic boxes to work as a dependable purchasing specification.
Specify the assembled working space
When specifying fluted plastic boxes, start with the product’s maximum working envelope, including any protective bag, projection or removable accessory. Add only the clearance needed for loading, unloading and manufacturing variation. State whether quoted dimensions are internal or external and whether the lid, divider and base insert are installed. A flat blank measurement cannot substitute for the available space in the erected container.
Measure the prototype after assembly using the intended closure method. Check more than the opening, because a base fold, wall joint or insert can reduce space lower in the box. Where the payload varies, include representative tolerance extremes in the fit trial. Keep the finished drawing tied to the actual product revision so that a later component change does not silently invalidate the packaging.
The decision should demonstrate that the box continues to assemble and close without damaged creases. An unexplained pass mark is less useful than the observation behind it.
Choose closure details around the operating cycle
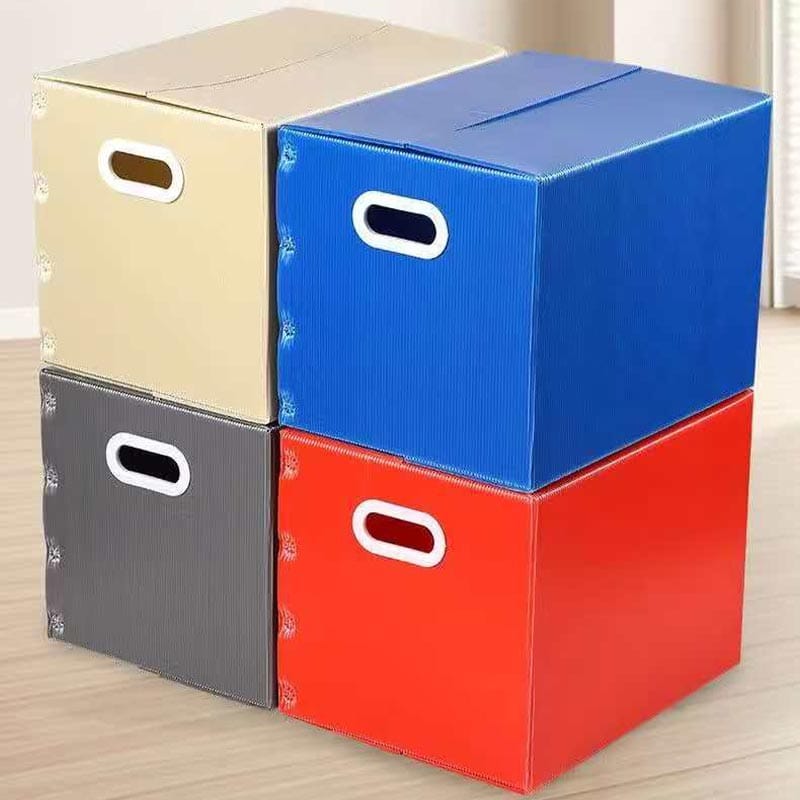
When comparing fluted plastic boxes, a closure has to work while the box is loaded, opened, cleaned, returned and reassembled. Compare tab engagement, straps, hook-and-loop fasteners or other details against the actual number of operations and expected contamination. Check whether operators can see that the closure is correctly engaged. Include gloves and normal work posture in the trial rather than evaluating the detail only on a desk.
Inspect attachment points after repeated use. Damage may begin around a rivet, slot or locally compressed channel before it becomes obvious at the main closure. Consider whether a worn closure can be replaced without discarding an otherwise usable box. Any replaceable item needs an identifiable part and a practical repair method, otherwise the theoretical repair advantage may not be realized in operation.
Keep the qualification focused on crease geometry and assembly sequence. Ask the supplier to explain deviations from the approved construction.
Calculate the fleet from complete loop time
For a project using fluted plastic boxes, a returnable container may be filling, in transit, waiting for unloading, awaiting collection, being cleaned or held for inspection. Count the entire loop when estimating the fleet. Peak demand and delays can matter more than the average outbound shipping rate. Track each stage separately during a pilot so that additional boxes are assigned to a real operating need.
Compare the number dispatched with the number returned in usable condition. Separate missing boxes from damaged boxes and boxes temporarily unavailable for cleaning. A lower purchase price does not compensate for a loop that loses packaging without a record. Use route or customer identifiers where practical, and agree responsibility at each handover before expanding the fleet.
In the operating trial, check whether fold lines fatigue before the packaging is retired. The relevant observation should determine the next design change.
Count all components in the empty return
When qualifying fluted plastic boxes, fold-flat boxes can reduce empty volume, but the return configuration must include lids, dividers, straps, inserts and any packing needed to keep them together. Measure a realistic return bundle instead of an isolated folded blank. Check whether workers can assemble the return load consistently and whether small reusable parts are likely to be lost.
Use the measured return package in the freight comparison. Include the labor required to collapse, sort and rebuild the packaging. If the return route is irregular, model the space required while empty containers wait for collection. The best arrangement is the one that fits the actual loop with manageable handling, rather than the one with the smallest theoretical folded dimension.
The reference sample should support one clear conclusion: the box continues to assemble and close without damaged creases. Preserve the conditions that made that result possible.
Use identification that survives the loop
Before ordering fluted plastic boxes, provide a clear location for the current part number, quantity and route information. Decide whether labels are disposable, removable or held in a reusable pocket. Scan barcodes on the loaded package under operating conditions. A label position that works on a flat sample can become hidden when boxes are stacked or placed on a shelf.
Remove or cover obsolete identifiers before the next load. Color can support identification, but it should not be the only distinction between similar parts. Check the marking method after cleaning and normal handling. Keep the box’s permanent asset identity separate from the changing contents label where the fleet needs to be tracked across several product types.
The buyer should be able to repeat the comparison and cycle a sample through the actual fold-flat and erecting routine. Use the same identification method for the production batch.

Build a small trial that represents normal work
When inspecting fluted plastic boxes, use the actual product, support, assembly method and handling sequence wherever practical. A simplified test is useful when it isolates a specific uncertainty, but record what it leaves out. Begin with a manageable quantity so unsuitable details can be corrected before tooling or a large order commits the project. Include the least favorable approved configuration when the product range varies.
Ask the people who will load, handle, print or inspect the item to participate. Their observations often reveal access and identification problems that a dimensional drawing does not show. Keep timing, damage and rejection observations distinct. A faster process is not an improvement if it leaves the protected product or finished graphic outside the agreed acceptance limits.
When reviewing a substitute, return to crease geometry and assembly sequence. Nominally similar material is only a candidate until the relevant checks are complete.
Separate a screening result from a service claim
For production using fluted plastic boxes, a short screening trial can compare candidates and reveal obvious weaknesses. It does not automatically predict performance through every transport, temperature or reuse condition. State what the trial demonstrates and where further evidence is needed. For packaging exposed to distribution hazards, use an appropriate complete-pack evaluation selected for the actual route and product rather than a convenient test with a familiar name.
Record the sequence of conditions, because cleaning before loading or loading before stacking can produce different results from isolated checks. Retain failed samples when they help explain a weakness. If a laboratory or specialist report is used, verify its configuration and scope before connecting its result to the intended order. Evidence is strongest when the tested construction matches the supplied one.
The priority for this project is crease geometry and assembly sequence. Keep it visible when comparing the candidates.
Keep the operating cost basis visible
When approving fluted plastic boxes, compare alternatives on the same function and usable output. Material price is only one input. Conversion yield, setup labor, rejected pieces, freight, cleaning and return handling may change the practical result. Include the costs that belong to the actual application and avoid adding speculative savings. Where an input is unknown, label it as an assumption and identify how a pilot could measure it.
For a reusable item, distinguish a completed usable trip from a dispatch that has not yet returned. Missing and damaged items should not vanish from the denominator. Update the comparison when route data becomes available. A transparent model with a few well-defined inputs is more useful than a precise payback claim based on a service life that has never been observed.
For the situation described here, cycle a sample through the actual fold-flat and erecting routine. Record the result before releasing the order.
Compare options for fluted plastic boxes
For fluted plastic boxes, compare the current construction, the proposed alternative and any reduced-material option against the same acceptance statement. Keep changes in dimensions, load arrangement and process conditions visible. The table is a project checklist rather than a claim that one standard grade fits every application.
| Requirement | What to record | How to judge the result |
|---|---|---|
| Application | a return loop that repeatedly collapses and rebuilds boxes | Use a production-equivalent configuration |
| Critical variable | crease geometry and assembly sequence | Agree a repeatable method before the comparison |
| Relevant risk | fold lines fatigue before the packaging is retired | Observe the actual operating stage where it begins |
| Trial | Cycle a sample through the actual fold-flat and erecting routine | Keep setup and sample identity with the record |
| Acceptance | The box continues to assemble and close without damaged creases | Record evidence and unresolved deviations |
| Reorder | Drawing revision, sample code and material identity | Compare the received batch with the approved reference |
Sources and related product information
Independent reference: ISTA. Use the relevant guidance with the project-specific qualification plan. This reference is not a test report or certification for a Zenlink product.
For available product formats, review Zenlink’s corrugated plastic product page and hollow-board product category. Ask which dimensions and modifications can be supplied for your drawing; availability and supporting documentation should be confirmed for the exact order.
Frequently asked questions
What should a buyer specify first for fluted plastic boxes?
Start with crease geometry and assembly sequence. Describe the finished use and identify the relevant drawing or product condition. For this project, the intended result is that the box continues to assemble and close without damaged creases.
Is nominal thickness enough to approve the material?
No. Thickness is one part of the construction. Review area weight where relevant, flute direction, conversion details and the actual operating function. Compare equivalent samples using the same method and acceptance criteria.
How should the first sample be tested?
The first trial should cycle a sample through the actual fold-flat and erecting routine. Record the sample identity, setup, conditions and observations. Review deviations before approving tooling or a larger order.
Can a similar-looking board be substituted without review?
A similar appearance does not establish equivalent behavior. Check the proposed change against crease geometry and assembly sequence and repeat the affected functional or dimensional checks before release.
What information helps Zenlink prepare a useful quotation?
Provide the drawing or finished dimensions, quantity, intended application, relevant material requirements, conversion details, delivery destination and the checks required for sample approval. Include a reference sample code or current packaging problem where available.
Discuss the specification with Zenlink
Send Zenlink the application drawing, required quantity and the issue you need to resolve. For fluted plastic boxes, highlight crease geometry and assembly sequence and describe the trial you expect to use. The team can review the relevant hollow-board or packaging format and discuss sample requirements for your project. Use the inquiry form below or the contact page to provide the working details.